Table of Contents
Bevel face width starts with a clearly defined application. The useful starting point is the production decision: what must the equipment deliver, how will the result be checked, and which supporting operations are required? This guide uses YL-PK95 as a relevant Yuanli product reference and separates published specifications from application conditions that require confirmation.
Bevel face width: the decision to resolve
A drawing may specify the sloping face length, the depth through the plate, or the horizontal setback. These dimensions are related but are not interchangeable. Before comparing a required groove with a machine's stated bevel width, mark the dimension direction on a cross-section. Also identify whether the angle is measured from the plate surface or from a square edge. An otherwise correct calculation can select the wrong machine when the reference changes. For production enquiries, provide both the drawing and the interpretation used in the calculation. Treat root face and opposite-side preparation as separate requirements, and ask the supplier to confirm the complete geometry rather than agreeing to an isolated width value.
Bevel face width: establish the cross-section and its references
In a bevel face width review, begin with a section drawing that shows the full joint or component, not only one isolated machined face. Identify the plate surfaces, datum, individual bevels, root face, and any mating part. State how each angle is referenced. An included angle formed by two edges is different from the angle on one prepared edge.
For bevel face width, make width direction visible directly on the drawing. The same dimension names must be used by engineering, the operator, the equipment supplier, and the inspector. If a drawing and a machine scale use different references, document the conversion rather than leaving it to memory. Check the interpretation with a sample cross-section before approving the production setup. This prevents a technically accurate cut from producing the wrong assembled geometry.
Bevel face width: plan the route through intermediate geometry
In a bevel face width review, a finished groove may require several machining stages, different orientations, or an approved secondary operation. Describe the intermediate condition after each stage and identify the datum used by the next. Keep the material left for later operations visible in the plan. A final dimension cannot explain whether an earlier pass removed the wrong supporting surface.
With bevel face width, the sequence must preserve remaining root face while allowing the required access. Discuss pass limits and permitted configurations with the equipment supplier. Do not extrapolate from maximum catalogue values to an untested combination of material and groove size. During a representative trial, record the adjustment sequence and inspect intermediate conditions where they affect the final result. This provides a route that another trained operator can reproduce.
Bevel face width: choose inspection points that reveal the problem
In a bevel face width review, inspection coverage should follow the physical risk of the feature. Include the beginning, middle, and end of a long edge where appropriate, together with corners or other transitions that may behave differently. Identify the measuring instrument, datum, and orientation so repeated readings are comparable. The required tolerances come from the approved drawing or fabrication specification.
For bevel face width, add a specific check for plate thickness range. Retain individual readings rather than only an average, because a local defect can disappear inside a satisfactory mean. If measurements disagree, first establish whether the inspection method is repeatable. A dispute about the gauge or reference cannot be solved by changing the machining setup blindly. Use the accepted sample and measurement record together when explaining the result to production.
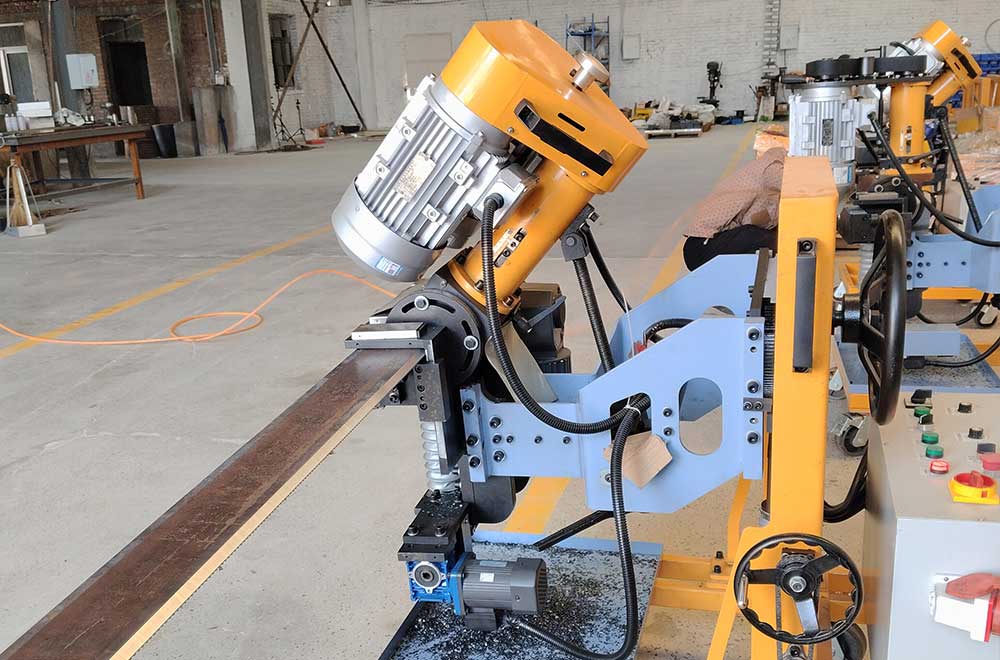
Illustration: define the triangle before calculating width
For an ideal straight bevel, let d be the depth through the plate and theta the angle between the sloping face and the original plate surface. The face length is d divided by sin(theta), while the horizontal setback is d divided by tan(theta). At 45 degrees and a hypothetical depth of 10 mm, the face is approximately 14.14 mm long and the setback is 10 mm.
This example is a geometry illustration, not a recommended joint design. If the angle is referenced to a square edge instead, the relationship must be interpreted accordingly. Real drawings may include a root face, unequal preparations, or other features. Show the supplier the dimension arrows so the required face width is compared with the correct catalogue quantity.
Bevel face width: application comparison checklist
Use this bevel face width checklist to compare a proposal with the required production condition. The rows are discussion and verification points; they are not universal machine settings or guaranteed acceptance limits.
| Review item | Question to resolve | Useful evidence |
|---|---|---|
| Width direction | Confirm width direction for the actual workpiece and order. | Annotated drawing, sample identification, or order-specific scope |
| Angle reference | Keep the requirement for angle reference identical across the options. | Supplier response with stated conditions and exclusions |
| Remaining root face | Observe remaining root face during the complete proposed work sequence. | Representative trial record, including supporting work |
| Plate thickness range | Record plate thickness range with an identified sample or configuration. | Repeatable inspection record or signed configuration detail |
| Single-pass limit | Assign responsibility for single-pass limit before release. | Named owner and agreed deliverable in the handover record |
| Final cross-section | Revisit final cross-section when the approved conditions change. | Updated application review with a documented decision |
Bevel face width: relevant Yuanli equipment
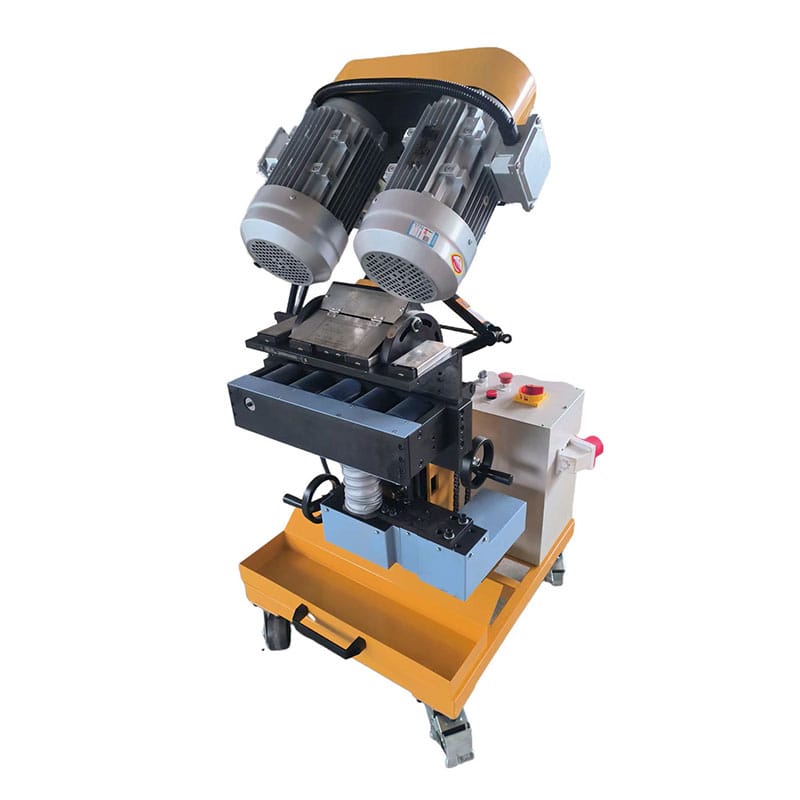
For bevel face width, the YL-PK95 product page provides a starting reference. Yuanli describes an edge-milling configuration for upper and side bevel preparation, with adjustable height and a floating-lift arrangement. Confirm the delivered configuration and the actual sample result before treating it as an approved production solution.
| Published item | Product-page reference |
|---|---|
| Motor power / power supply | 6,000 W / 380 V / 50 Hz |
| Plate thickness range | 4–95 mm |
| Bevel angle | 0°–75° (adjustable) |
| Groove types | K-, V-, X-, and Y-grooves; upper bevels; 0° side milling |
| Bevel width | 20 mm per pass; up to 70 mm with multiple passes |
| Machine weight / dimensions | Approx. 300 kg / 0.7 × 0.7 × 1.5 m |
Published limits describe reference specifications; they do not establish that every maximum can be used simultaneously. Confirm the material, geometry, tooling, support, and delivered options for the intended job.
Bevel face width: prepare a technical enquiry
A useful bevel face width enquiry combines the workpiece drawing, material identification, incoming condition, expected order pattern, and the acceptance requirements. Add photographs that show the relevant geometry, with dimensions or an identified reference where needed. Include width direction and final cross-section explicitly so the supplier can respond to the actual decision.
Compare the model above with the Yuanli beveling machine range. Ask which proposed conditions have already been demonstrated and which require samples. If the scope changes during discussion, update the enquiry and keep the revised requirements with the quotation.
For terminology used in joint cross-sections, see the TWI explanation of weld-joint preparation geometry; the applicable joint dimensions still come from the approved fabrication drawing and procedure. For related Yuanli guidance, review the existing groove-inspection guide.
Ready to discuss bevel face width for your production line? Contact Yuanli with the application package above and request a configuration review, sample-trial scope, and quotation. Use the enquiry form below to describe the job and the result you need.
Frequently asked questions
What should be defined first for bevel face width?
Start with width direction and angle reference. Connect them to the actual drawing, workpiece condition, and required result. The relevant model can then be evaluated against a specific application instead of a general product description.
Which evidence is useful when reviewing bevel face width?
Request an identified sample or configuration record covering remaining root face and plate thickness range. Preserve the method, observations, and any deviations. A selected photograph or a single nominal specification cannot replace the complete agreed verification.
Is YL-PK95 automatically suitable for this application?
No. The YL-PK95 page is a product reference for the bevel face width discussion. Suitability depends on the material, complete geometry, required output, supplied configuration, and the representative evidence accepted by the buyer and supplier.
Can bevel face width be approved from a catalogue alone?
A catalogue can support initial screening, but it does not establish every condition of the intended job. Resolve single-pass limit and final cross-section before release. Use a representative trial whenever the required result or supporting method remains uncertain.
What should I send Yuanli about bevel face width?
Send the relevant drawing, material and incoming-condition details, expected quantities, and the acceptance criteria. Identify width direction, remaining root face, and any unresolved constraint. Request a written response with the recommended configuration and any conditions requiring a sample trial.